
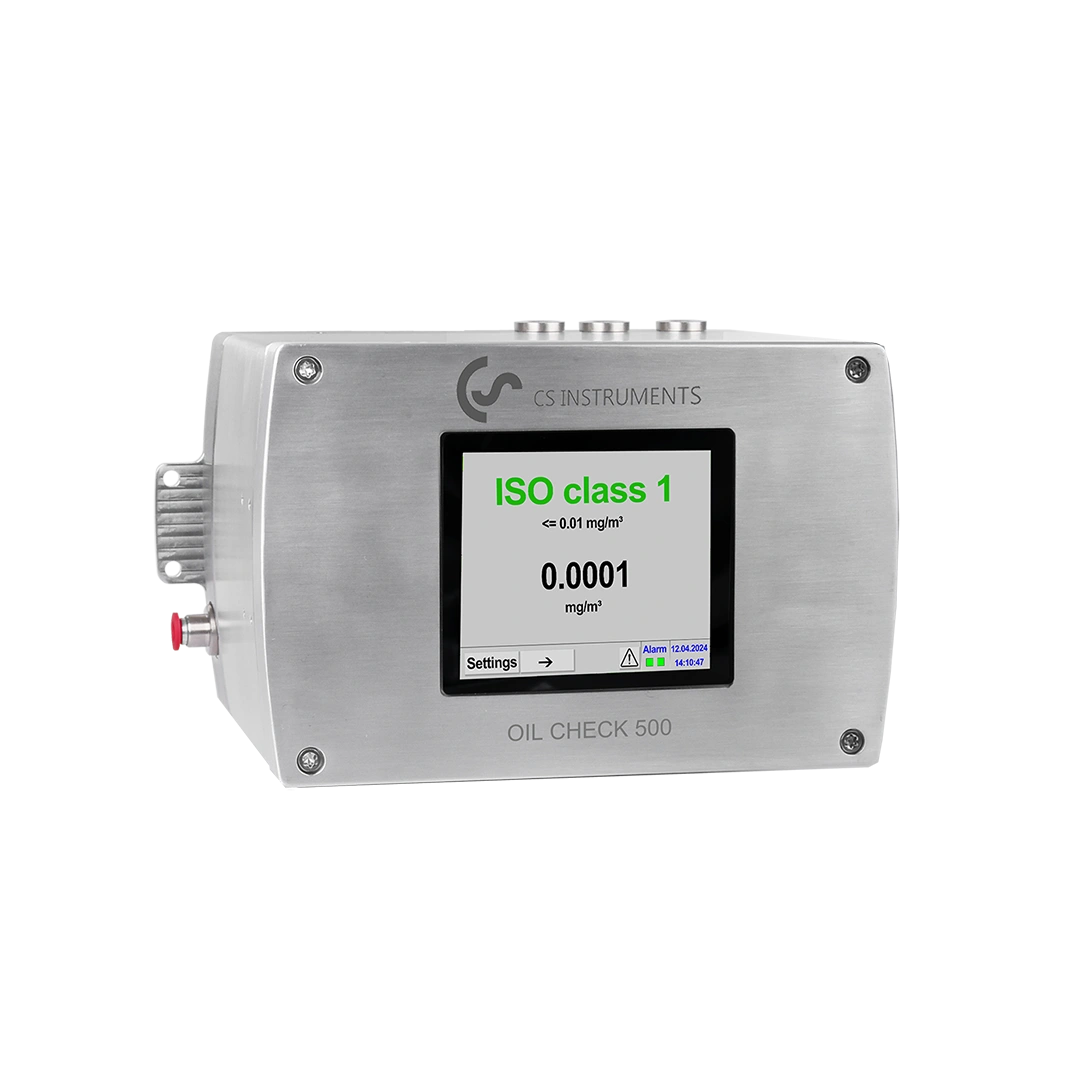
OIL CHECK 500 – Analyser for residual oil vapours in compressed air and gases
Maximum safety thanks to maximum sensitivity - continuous monitoring of the critical parameter vaporous residual oil content in accordance with ISO 8573.
An oil-free compressor prevents additional oil ingress from the compression stage. Only measurement can reveal the actual behaviour of the vapor-phase residual oil content. An indicative PID measurement in accordance with ISO 8573-5 impressively highlights changes during operation.
Two customer measurements demonstrate what a PID-based analyzer can achieve when measuring the vapor-phase residual oil content. In the first case, it reveals how the measured value changes when the intake is switched. In the second case, distinct oil vapour signatures from the individual compressors were identified across three oil-free compressors connected to a common manifold. Together, these cases demonstrate how an indicative measurement can support the assessment of the treatment process and the monitoring of individual compressors.
This gives operators three practical approaches:
At a drinks manufacturer, the intake configuration of a system with an oil-free compressor was switched from external to internal intake. The OIL CHECK 500 clearly shows a difference in the measured value following media treatment: 0.003 mg/m³ for external intake and 0.006 mg/m³ for internal intake.
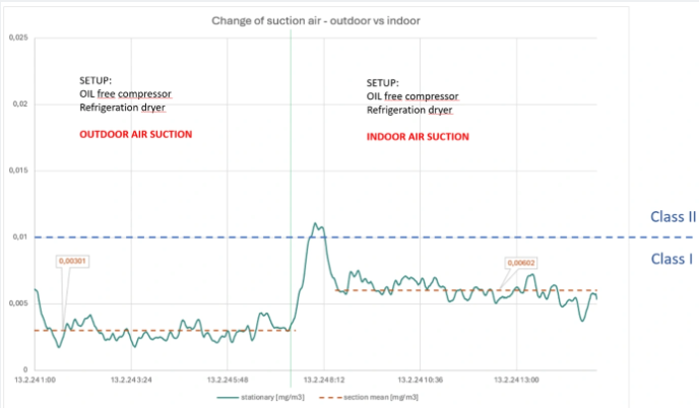
The measurement trend thus demonstrates that the intake conditions were reflected in the measured oil vapor content. Such data can help to assess the treatment process under real operating conditions and to correlate changes with the plant’s operating status. This supports data-driven decisions regarding process control and maintenance.
In a second customer case, three oil-free compressors connected to a common manifold were monitored. During the measurement, the operating phases alternated: at times, one compressor ran continuously whilst a second compressor ran intermittently, followed by a third unit.
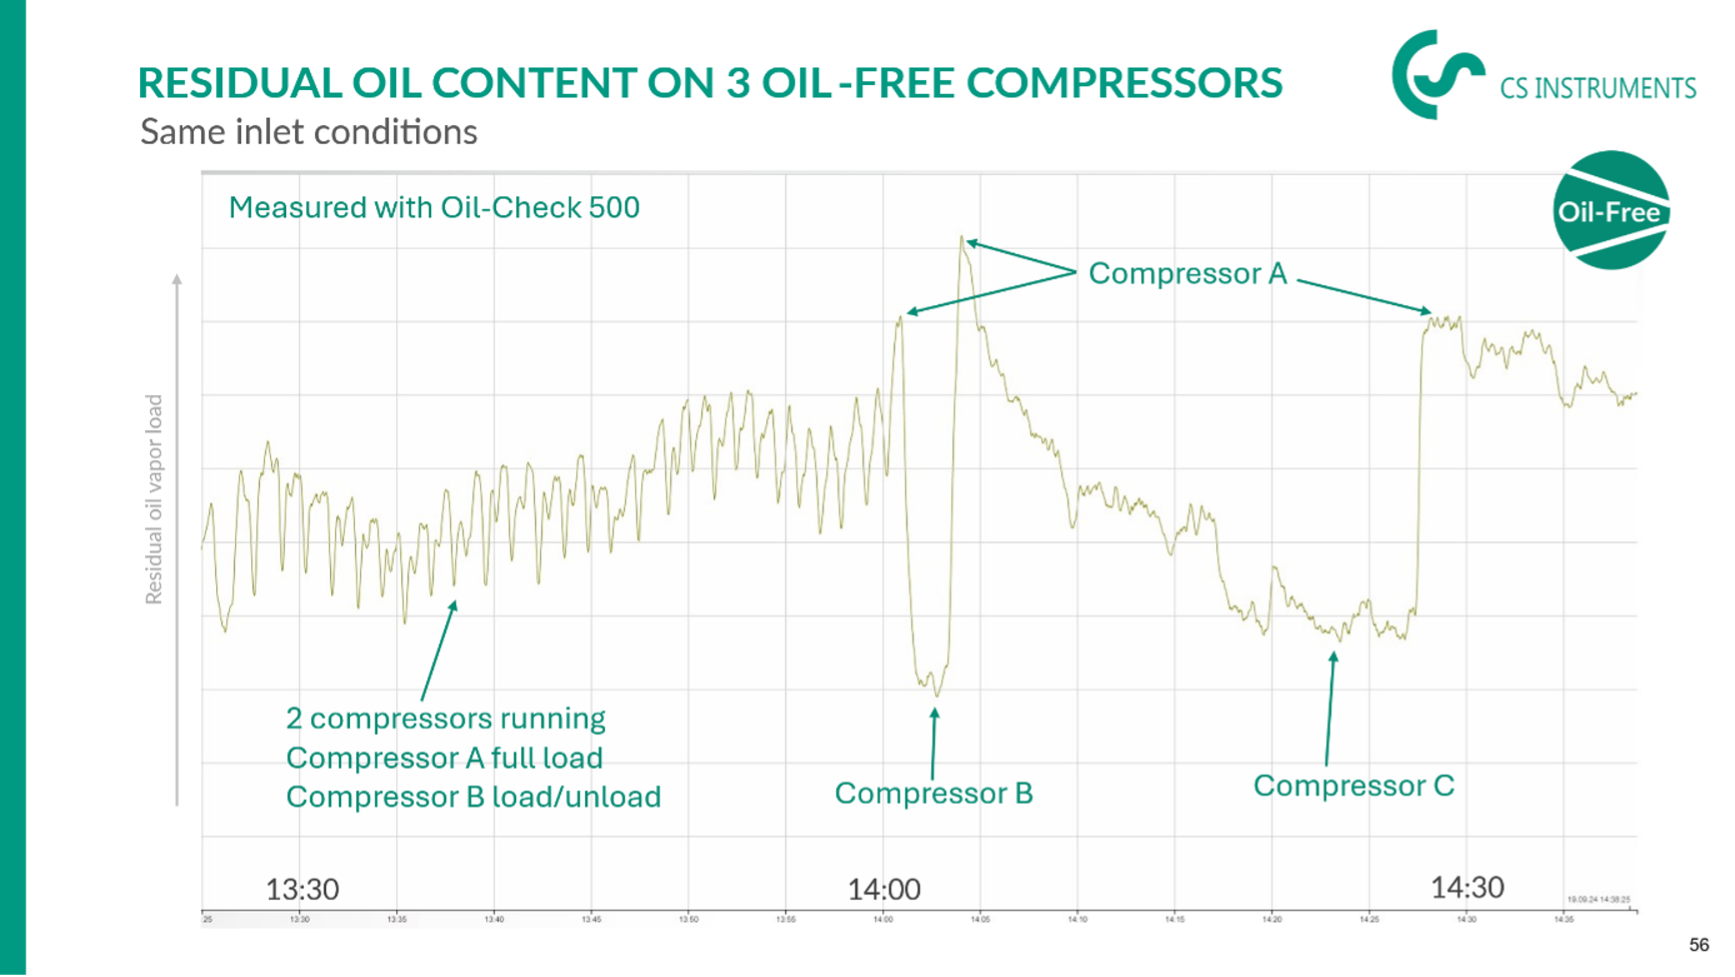
The measurement curve shows distinguishable oil vapour signatures for the individual compressors during these phases. This enabled the compressors to be assessed and monitored individually on the basis of their respective measurement profiles. This is particularly noteworthy as it demonstrates the level of detail achievable in monitoring and analysis through the indicative measurements provided by the OIL CHECK 500.
‘Oil-free’ primarily describes the principle of compression. It is not a continuous measured value for compressed air quality. Intake air, ageing and the rest of the compressed air system can influence the measured concentration.
The compressor is only one part of the compressed air system – ‘oil-free’ does not automatically mean a measured value of zero.
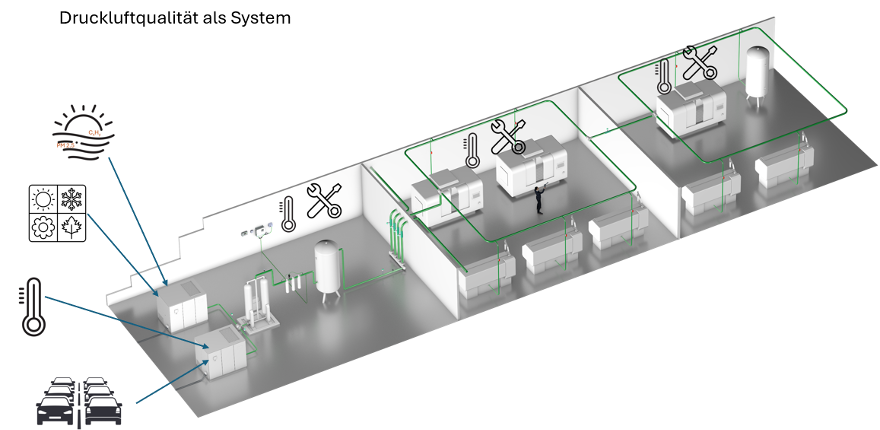
The key point is this: the compressed air system is not static. It is directly connected to its environment and must cope with a multitude of changing influences.
The OIL CHECK 500 detects the vapor-phase component and performs an indicative photoionization detector measurement in accordance with ISO 8573-5:2025.41 The continuous measured values reveal trends over time and can supplement laboratory analyses. However, they do not replace the reference method for standard-based classification. Furthermore, the photoionization detector measurement does not automatically detect all oil phases, such as aerosols or liquid oil.
Would you like to find out whether indicative residual oil vapor monitoring is suitable for your plant? Book a personal consultation.

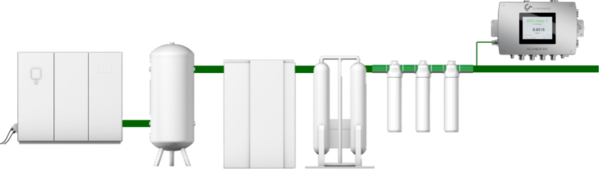
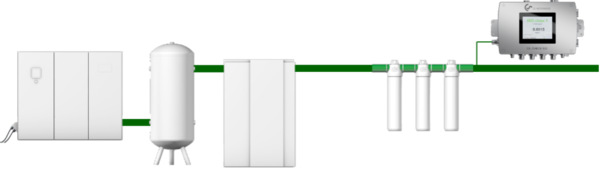
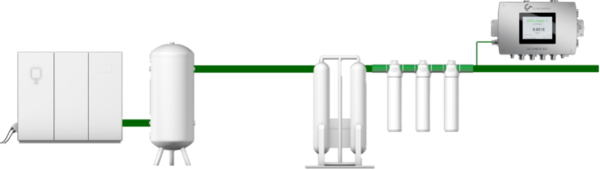
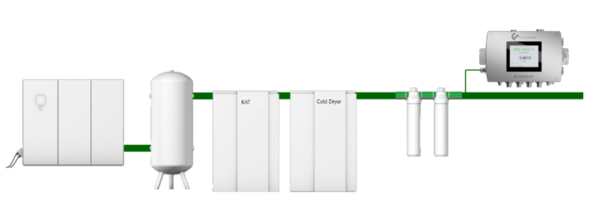
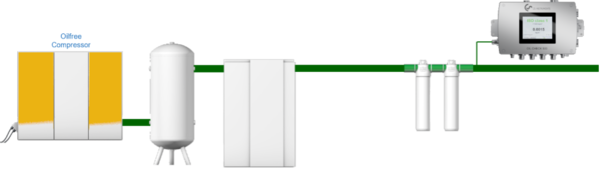
| SCENARIO | PERMITTED |
(1) Compressor, (2) Tank, (3) Refrigeration dryer, (4) Desiccant dryer, (5) Filter stage incl. Act. Carbon |  |
(1) Compressor, (2) Tank, (3) Refrigeration dryers, (4) Filter stage with activated carbon | |
(1) Compressor, (2) Tank, (3) Desiccant dryer, (4) Filter stage with activated carbon | |
(1) Compressor, (2) Tank, (3) Catalytic converter, (4) Refrigeration dryer, (5) Filter stage | |
(1) Oil-free compressor, (2) Tank, (3) Refrigeration dryer, (4) Filter stage | |
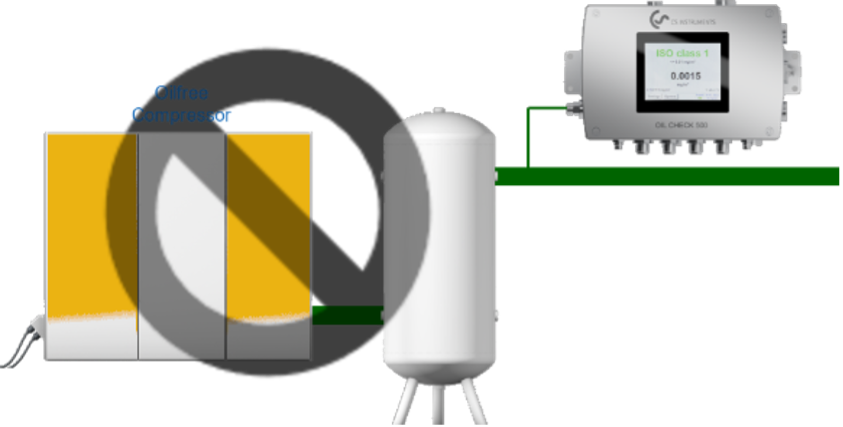
| SCENARIO | NOT PERMITTED |
(1) Oil-free Compressor, (2) Tank, (3) OIL CHECK 500 |  |
(1) Compressor, (2) Tank, (3) OIL CHECK 500 | |
Would you like to continuously monitor the quality of your Compressed air?
Use the OIL CHECK 500 to continuously monitor your Compressed air quality and ensure that your production always meets the highest standards. You can find more information on the product page or call us for a personal consultation and customised solutions for your compressed air monitoring. Take the initiative now and optimise your production processes!
Maximum safety thanks to maximum sensitivity - continuous monitoring of the critical parameter vaporous residual oil content in accordance with ISO 8573.

Ideal instrument for dew point measuring for all kinds of dryers.

The high-precision, optical particle counter measures particles from a size of 0.1 µm and is therefore suitable for monitoring compressed air quality class 1 ISO 8573.