
VA 550 - Thermal mass flow sensor for flow measurement
Insertion sensor for demanding industrial applications, comes with ATEX + IECEx approval for Ex zones or DVGW approval for use in natural gas.
Author: Florian Buchner
Position: Product Manager, Flow Measurement Technology
Area of Expertise: Thermal flow measurement, industrial gas measurement, and energy monitoring
Last updated on October 14, 2026
At a Glance: Thermal mass flow meters from CS INSTRUMENTS measure natural gas consumption without moving parts and directly output the standarized volume flow—for consumption monitoring, cost center tracking, and energy management. The VA 550 and VA 570 are available, depending on the model, with ATEX approval or DVGW approval for natural gas (up to 16 bar).
Industrial natural gas networks typically use turbine meters, piston gas meters, and quantometers; users sometimes refer to them generally as impeller meters. If low flow rates are not measured accurately, moving parts require maintenance, or digital consumption data is lacking, a thermal mass flow meter for natural gas is an alternative worth considering.
How turbine-wheel and rotary-piston gas meters work—and where their limitations lie. In a turbine-wheel gas meter, the gas flow strikes a mechanically mounted turbine wheel and drives it; the rotational speed is proportional to the flow velocity and, given the known pipe cross-section, to the volume flow. In a rotary piston gas meter, the pressure difference drives rotors in a measuring chamber, each of which encloses a precisely defined volume of gas and conveys it to the consumer. The usable measuring range of mechanical gas meters depends heavily on the design, size, operating pressure, and model: Simple quantometers often operate with significantly lower dynamic range than a thermal sensor.
The inherent limitations of both designs stem from their moving parts: Bearings age due to dirt or abrasion and cause measurement deviations; exceeding the measurement range can cause bearing damage; some bearings must be lubricated regularly—which is easily neglected in practice—contaminated gas leads to greater deviations, and cleaning is virtually impossible; in the case of rotary piston gas meters, there is also a design-related pressure loss.
| Criterion | Turbine-wheel meter / Quantometer | Thermal mass flow meter |
| Measured variable | Typically operating volume | Mass flow, from which standard volume is derived (e.g., according to DIN 1343, 1013.25 mbar; 0°C) |
| Moving parts | Yes | No |
| Low flows | Depending on design | High dynamic range possible (up to 1:1000) |
| Pressure drop | High | negligibly low |
| Standard volume | Volume converter + pressure and temperature compensation required | Directly, if parameterized correctly |
| Digital integration | Depends on the device | Depending on the model: Modbus TCP, Modbus RTU, M-Bus, IO-Link, HART, etc. |
| Retrofitting large pipelines | Complex | Insertion type sensor possible |
Measuring partial load and peak flow: The VA 550 and VA 570 offer a measuring span of up to 1:1000. The actual minimum and maximum flow rates (Qmin/Qmax) remain the decisive factors. With the VA 550 and VA 570, the measuring range can be selected to suit the application (Low Speed, Standard, Max, and High Speed). Additional advantages of the thermal principle include negligible pressure loss and the ability to measure extremely low consumption rates: The VA 550 and VA 570 are very often used in large pipe cross-sections with low gas consumption, where mechanical gas meters reach their limits.
Prevent rotor wear: The thermal principle measures based on the heat dissipation of a heated sensor—without rotor bearings and with minimal additional pressure loss. The sensors (heater and temperature sensor) are designed for harsh industrial environments and housed in a thin, robust stainless steel tube: no bearings, no wear, easily accessible, and simple to clean if contaminated. The devices are very robust and virtually maintenance-free.
Output standard volume directly: Mechanical gas meters are typically operating volume meters; conversion to standard volume is performed by external volume converters equipped with additional pressure and temperature sensors. To achieve the required accuracy, these sensors must be highly precise and located inside or near the meter—their measurement errors are added to the meter’s accuracy, which is typically specified in operating volume. The VA 550 and VA 570 measure the thermal mass flow rate and, with appropriate gas parameterization and specified reference conditions, directly output the standarized volume flow; a separate volume converter with additional pressure and temperature measurement is not required for this. For comparisons, the reference conditions must match (e.g., 0 °C; 1,013.25 mbar (a) per DIN 1343—also referred to as standard m³/Nm³); for kWh calculations, the calorific value is added.
At elevated operating pressure, the standard volume is greater than the operating volume—in proportion to the absolute pressures, with an additional correction for temperature. If an operating volume is incorrectly reported as a standard volume or processed as such, the actual gas consumption is systematically underestimated, and the kWh balance mirrors this error exactly because it depends linearly on volume:
| Operating overpressure | Ratio of standard volume to operating volume (ideal gas, without temperature term) | Underestimation due to confusion |
| 50 mbar | ≈ 1.05 | ≈ 5% |
100 mbar | ≈ 1.10 | ≈ 10% |
| 500 mbar | ≈ 1.49 | ≈ 33% |
| 1 bar | ≈ 1.99 | ≈ 50% |
| 4 bar | ≈ 4.95 | ≈ 80% |
In addition, there is the temperature factor: there is a difference of approximately 7% between a gas temperature of 20 °C and the standard reference temperature of 0 °C. These values are provided for illustrative purposes using an ideal gas; for billing or highly accurate state conversion, factors such as temperature, gas composition, and compressibility must be taken into account (DVGW Regulation G 685). The most common source of error in energy balances is not measurement precision, but an unnoticed incorrect volume reference.
In main and distribution lines, a point of measurement continuously monitors the total consumption of a building, area, or boiler room—for larger existing pipelines, the VA 550 is a good option as an insertion type sensor because it eliminates the need to install a complete inline measuring section in the nominal diameter. Directly upstream of individual consumers (boilers, burners, production facilities), it becomes clear which consumer requires how much natural gas and when—the basis for load profiles and cost centers. The most informative approach is the combination: main measurement plus submeters shows total consumption and its distribution.
With many installed mechanical meters, consumption data is transmitted solely via a pulse output; modern electronic meters can also offer digital interfaces. Depending on the ordered configuration, the VA 550 and VA 570 can be integrated directly into the central control system or energy monitoring software via Modbus TCP interface over Ethernet (flow, total consumption, gas temperature); an RTU/TCP gateway is not required. Optional Power over Ethernet combines data transmission and power supply in a single network cable—this reduces installation effort, especially when multiple points of measurement are involved. Alternatively, Modbus RTU, 4…20 mA, pulse, M-Bus, IO-Link, or HART are available.
Retrofitting the VA 550 as an insertion type sensor: The sensor is installed via a suitable process access point or ball valve. A depth scale and defined orientation ensure a reproducible sensor position. The VA 550 is designed for operating pressures up to 50 bar (DVGW version up to 16 bar); installation and removal under pressure are performed via a ½" ball valve with a retaining ring.
VA 570 as an inline solution: During cleaning or recalibration, the measuring section remains in the line—only the sensor unit is removed. For recalibration, the sensor is sent in; replacement sensors can be installed for the duration of the calibration, ensuring no interruption in operation.
Operation: On the VA 550 and VA 570, optical keys allow settings to be adjusted without opening the housing—the operation of both devices is identical. Digital device and status information (Modbus registers) support troubleshooting and handover documentation.
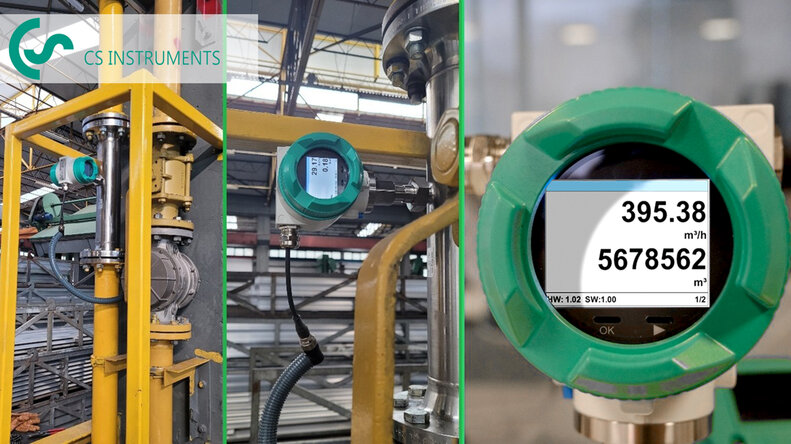
In a boiler application, 330 Nm³/h of natural gas and 5,000 kg/h of vapor are measured. The boiler efficiency is calculated from gas consumption, heating value, and steam data—84% in the documented example. In this way, a simple consumption measurement is transformed into a reliable metric for efficiency and maintenance. (→ Steam Boiler Application Report)
| sensor | Classification |
| VA 570 | Inline with integrated measuring section—flanged versions nominal diameter 15–80, threaded versions ½"–2"; operating pressure 16 bar (special version 40 bar); Measuring head removable for calibration; measuring section remains in the pipe with a sealing cap; ATEX/IECEx or DVGW compliant, depending on the version. |
VA 550 | Insertion type sensor for larger and existing pipes – particularly suitable for retrofits via a suitable measurement connection; ATEX/IECEx or DVGW compliant, depending on the version. |
The VA 550 and VA 570 are available with ATEX approval/IECEx approval depending on the variant; the Ex marking for these variants, according to the data sheet, is: ATEX II 2G Ex db IIC T4 Gb (gas) and II 2D Ex tb IIIC T90 °C Db (dust); IECEx Ex db IIC T4 Gb / Ex tb IIIC T90 °C Db. The Ex version is rated for a medium temperature of up to 120 °C and has an IP 65 protection rating. The EU-type examination certificate is available in the download section. It is the operator’s responsibility to verify suitability for the specific explosion-protected area. CS INSTRUMENTS provides technical data sheets and Ex certificates for this purpose but does not assume any advisory role regarding zone classification or suitability for a specific facility.
Note on Explosion Protection: A safe point of measurement requires a suitable device, proper installation, and the necessary tests. For electrical Ex systems, the applicable DIN EN IEC 60079-14 (VDE 0165-1) standard must be observed in particular. Risk assessment, zone classification, and the explosion protection documentation are the responsibility of the employer or operator within the scope of their respective legal obligations and must be prepared by qualified personnel. This article provides information on equipment characteristics; it does not constitute advice and is not a substitute for a facility-specific explosion protection assessment. The selection, use, and installation of the measuring technology are the responsibility of the facility operator or the qualified companies or individuals commissioned by the operator. The device design, type plate, operating instructions, and approval conditions—including special “X” conditions—are binding.
The VA 550 and VA 570 have not been assessed for conformity as measuring devices for gas billing subject to legal metrology; they are intended for operational consumption, process, and energy measurements. For measured values used in commercial transactions, the applicable requirements of the MessEG/MessEV and—where applicable—the MID (gas meters and volume converters, MI-002) apply; a calibration certificate alone is not sufficient. According to the data sheet, the accuracy for operational measurements is ±1.5% of the measured value ±0.3% of the upper range value (Standard) or ±1.0% of the measured value ±0.3% of the upper range value (Precision version).
No. It measures the mass flow rate and, given appropriate gas parameters and specified reference conditions, directly outputs the standarized volume flow; there is no need for separate pressure and temperature conversion. This requires that the reference conditions match those of the energy management system.
The thermal principle depends on the gas composition. Gas parameters, calibration gas, and, if applicable, actual gas calibration (optional feature) are specified at the time of ordering; the operator must provide the gas composition and variation range—especially prior to a gas switchover.
This is determined by a competent risk assessment of the facility, not solely by the medium—it is the operator’s responsibility to verify suitability for the specific explosion-protected area.
Because the standard volume is greater than the operating volume at overpressure—in proportion to the absolute pressures: about 10% at 100 mbar overpressure, and about twice that at 1 bar. Without a volume converter or direct standard volume output, this error is factored linearly into the kWh balance. In addition, the gas temperature significantly affects the gas density and thus the volume.
Not necessarily. For inline replacement, the overall length, the connections, and the installation conditions are the decisive factors; the plug-in version often circumvents these. Prerequisites include clean, non-condensing gas, correct parameterization, and suitable supply and exhaust lines—a brief sketch of the measurement point indicating the length of the supply line facilitates the design.
Insertion sensor for demanding industrial applications, comes with ATEX + IECEx approval for Ex zones or DVGW approval for use in natural gas.

ATEX + IECEx approval for Ex zones and DVGW approval for use in natural gas.